Rotary bottle unscrambler machinery for UK packaging lines
01Stable infeed
Reduce manual bottle correction before fillers, cappers and labellers.
02Line-ready layouts
Review transfer height, conveyor interface, accumulation and guarding early.
03Real bottle testing
Match the machine route to bottle diameter, height, material and stability.
Industrial bottle handling
Stop the infeed from limiting the rest of the production line.
Manual bottle placement often becomes the weak point once filling, capping and labelling equipment is upgraded. A correctly specified bottle unscrambler gives the downstream machinery a steadier stream of containers and reduces operator intervention.
The right choice depends on more than speed. Bottle shape, base stability, available footprint, conveyor height, accumulation, future formats and downstream controls all affect the final specification.
A professional specification starts with the bottle, not a brochure.
1
Confirm bottle data
Diameter, height, base shape, material, empty weight and stability define the feeding method.
2
Map the line
Check conveyor height, downstream machine speed, available footprint, access and guarding.
3
Match real output
Specify for production flow, changeovers and bottle behaviour rather than headline machine speed alone.
4
Plan integration
Review accumulation, transfer rails, controls and operator loading so the line runs consistently.
Applications
Built around production environments that need reliable empty-bottle flow.
Contract packing
Multi-format projects with frequent bottle and product changes.
Food, drink and household
Bottle infeed before filling, capping, labelling and coding stages.
Cosmetics and pharma-style packs
Small containers where presentation and downstream stability matter.
Buyer questions
Clear answers before you request a quote.
What does a bottle unscrambler do?
It receives empty bottles in bulk or semi-bulk form and presents them in a controlled stream for downstream machinery such as fillers, cappers and labellers.
Is a rotary feed table the same as a bottle unscrambler?
A rotary feed table can provide simple bottle accumulation and feeding. A full automatic bottle unscrambler may add more controlled orientation, outfeed and automation depending on bottle geometry and required speed.
Can it be added to an existing line?
Yes, provided line height, footprint, transfer point, conveyor width, guarding and electrical requirements are checked before specification.
What information should be sent for a quote?
Send bottle diameter, height, material, sample photos, target output, downstream equipment details, conveyor height and available floor space.
Machine selection evidence
Compare the route against bottle geometry, line speed and available space.
Published machine figures are a starting point. The final bottle unscrambler route should also be checked against real sample bottles, the way bottles are loaded, the transfer into the next conveyor and the changeover range expected in production.
Route
Verified published data
Useful starting point
Changeover and layout checks
LU-LP150 automatic bottle unscrambler
30–60 bottles/min; bottle diameter 20–100 mm; bottle height 20–150 mm; 220V 50Hz; about 1100 × 1616 × 1163 mm; about 260 kg.
Small plastic bottles where manual arrangement is restricting the filling, capping or labelling line.
Confirm the smallest and largest bottle, guide adjustments or dedicated change parts, outfeed direction, guarding and operator loading access.
LU-SP800 rotary bottle unscrambler
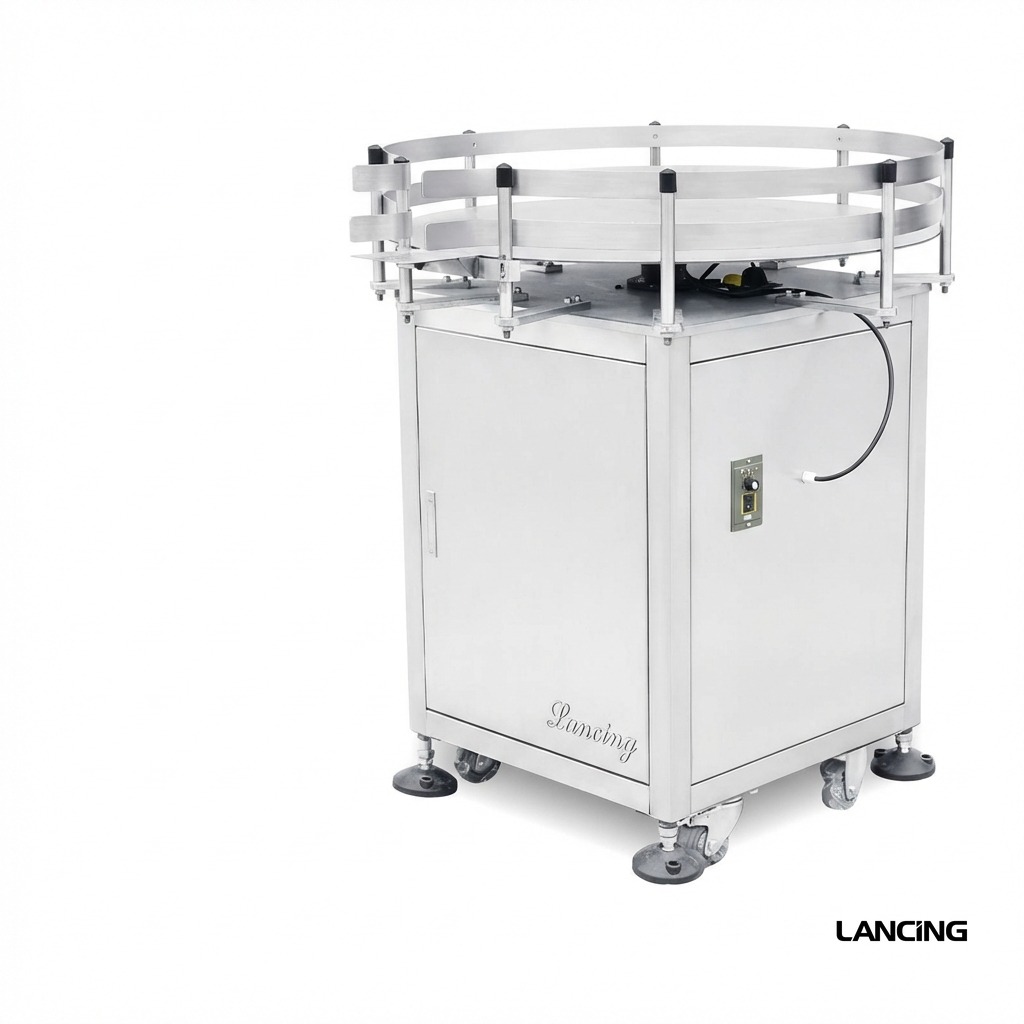
2400–3600 BPH; 800 mm turntable at 10 rpm; bottle diameter 20–100 mm; bottle height 30–120 mm; 850 × 850 × 1500 mm; 50 kg.
Stable bottles needing compact accumulation and controlled delivery into downstream equipment.
Confirm bottle stability on the rotating disc, available footprint, conveyor height, guide rails and whether the bottle needs orientation rather than simple feed.
Send enough information to test stability, presentation and recovery.
The strongest enquiry brief allows the bottle infeed to be assessed as part of the working line rather than as an isolated catalogue machine.
Bottle drawings, photographs and representative empty samples
Diameter, height, material, empty weight and base geometry
Required sustained output and the downstream machine rate
Conveyor height, width, direction and available floor space
Changeover range and whether dedicated change parts are acceptable
Trial evidence for tipping, scuffing, jams, restart and downstream transfer
Related Lancing routes
Find guidance for other parts of the packaging line.
BottleUnscramblers.co.uk remains focused on bottle unscrambling, orienting and feeding. Use the related Lancing sites when the project brief is principally about conveyors, rinsing, closure feeding or a complete packaging line.
Use this route when filling, capping, labelling, conveyors, controls and handover need to be planned as one line.
Decision path
Choose the next check from the first bottle-handling problem.
Start with the first observable bottle-handling problem, then collect the evidence needed by the page that owns that decision. This keeps bottle-shape and problem research connected to the strongest commercial or technical page instead of treating each search phrase as a separate machine.
First observable problem
Evidence to collect
Strongest next page
Decision to close
Manual bottle arrangement is limiting output
Representative bottles, sustained downstream demand, loading method and outfeed condition.
Whether the retained equipment can support the new bottle-handling duty.
When more than one risk applies, start with the governing extreme rather than the most common bottle. A bottle family may be mostly stable but still require a different route because one lightweight, tall or presentation-sensitive format controls the changeover design. Record that governing format in the enquiry and keep the supporting sample, video and settings evidence with the owner page used for the decision.
Final project readiness
Move from a machine shortlist to an evidence-backed acceptance brief.
The strongest bottle-unscrambler enquiry connects the chosen route to the bottle family, the line interface and the evidence that will be used at trial, FAT and production handover.
Decision
Evidence to prepare
Strongest owner page
Acceptance outcome
Automatic or rotary route
Smallest, largest, lightest and least stable bottle; sustained line demand; available footprint.
A clear boundary between the bottle infeed package and the equipment it supplies.
Project evidence pack
Keep one controlled record from enquiry through production handover.
Approved bottle schedule with dimensions, materials and representative samples
Line-layout drawing with conveyor heights, direction and operator access
Machine-route decision and any change-part assumptions
Sample-trial, orientation-video and surface-inspection records
Jam, stop, restart and downstream-transfer evidence
Final settings sheet, open-items register and production handover sign-off
Buyer questions
Questions that identify the right bottle infeed route.
Use these questions to decide whether the line needs a bottle unscrambler, a compact rotary feed route or a wider conveyor and controls review.
How can you tell whether bottle infeed is the real line bottleneck?
Bottle infeed is likely to be the real bottleneck when the filler, capper or labeller repeatedly waits for bottles even though it still has available capacity. A second sign is that output improves immediately when an operator manually uprights, spaces or pushes bottles through the infeed. Confirm this with a short observation record rather than relying on one stoppage.
Record where the first abnormal event occurs, whether the downstream machine is calling for bottles, and whether the bottle stream contains gaps, surges, tipping or manual corrections. The bottle unscrambler working-principle guide explains the stages to inspect, while the line integration page covers the interfaces around the machine.
What makes a bottle a good candidate for a compact rotary feed route?
A compact rotary route is most credible when the empty bottle has a stable base, moves predictably around the table or disc, and does not require complex positive orientation before discharge. Tall, very light, soft, handled or strongly shaped bottles may still work, but they need representative trials because centre of gravity, guide contact and back pressure can change the result.
The decision should be based on the least stable production bottle, the real transfer height and the downstream demand. Compare the route categories in rotary table versus centrifugal-disc unscrambling before treating a headline capacity as proof of suitability.
What should be prepared before asking for a bottle unscrambler shortlist?
Prepare the complete bottle set, not only one convenient sample. Include dimensions, material, empty weight, photographs, target sustained output, conveyor height, available footprint, downstream machinery and expected changeovers. Also state whether visible scuffing, bottle orientation, operator loading height or retained existing equipment creates a specific acceptance requirement.
A simple layout sketch and photographs from the operator side, service side and transfer point remove avoidable assumptions. Use the site-survey requirements and supplier-question guide to prepare the first technical discussion.
Can a bottle unscrambler be selected from bottles per hour alone?
No. Bottles per hour is only one input because usable output also depends on bottle geometry, stability, format change, replenishment, downstream stops and the transfer into the next machine. A short burst at the outfeed is not the same as a sustained production result. The bottle and line conditions used to support the figure must be recorded.
The existing line-speed guide explains the difference between nominal and sustainable demand. Acceptance should then be tied to the agreed bottle set and the checks in the FAT and SAT guide.
Project-stage routes
Move from the current line problem to the right evidence page.
Use the project stage to choose the next technical page rather than comparing machine names without the supporting bottle and line information.
Use the supplier-question guide to compare scope, evidence, exclusions and acceptance on the same basis.
Week 2 buyer questions
Questions that narrow the bottle infeed route before quotation.
Use these questions to identify the governing bottle, the true bottleneck and the evidence required before a machine route is selected.
Which bottle information determines whether a rotary or automatic route should be shortlisted?
The machine route is decided by the complete bottle and line brief: bottle diameter, height, material, empty weight, base stability, neck and shoulder geometry, required sustained output, conveyor height and downstream machine. A compact rotary route may suit stable bottles that only need controlled delivery, while an automatic route is considered when bulk loading and bottle arrangement are the main constraints. Use the machine comparison and buyer guide together before requesting a quotation.
How can a buyer tell whether the bottleneck is manual loading or the transfer into the line?
Record where the first abnormal bottle movement occurs. If the operator cannot place enough bottles to keep the next machine supplied, manual loading is the likely constraint. If bottles are available but tip, queue, hesitate or jam at guides and transfer points, the interface is the stronger suspect. A short video covering loading, accumulation, transfer and downstream demand is more useful than filming only the final pile-up.
Which line-speed figure should be used when specifying a bottle unscrambler?
Use the sustained bottle demand that the production line must achieve, not a short peak or the maximum nameplate speed of one downstream machine. State the normal bottles-per-minute target, expected stops, changeovers and whether the downstream line runs continuously or intermittently. The selected route should maintain the required supply without creating damaging back pressure, repeated stop-start cycling or an unstable bottle queue.
When is a representative bottle sample trial essential?
A representative trial is especially important when bottles are lightweight, tall, soft, tapered, flat-sided, oval, prone to static, visually sensitive to scuffing or spread across a wide format range. It is also needed when the machine must recover after planned stops or when the transfer point is difficult to predict from drawings. The trial should use the governing bottle formats, not only the easiest bottle.
What should be included in the first bottle unscrambler enquiry?
Include clear bottle photographs, dimensions, material, empty weight, the smallest and largest formats, target sustained output, downstream machine type, conveyor height, available footprint and a description of the current infeed problem. Add a layout or short line video where possible. This lets Lancing UK distinguish a rotary feeder, automatic unscrambler, conveyor improvement or sample trial before a detailed proposal is prepared.
Questions that close the gap between machine selection and daily production.
These questions cover the loading method, operator access and production records that should be agreed before the bottle infeed is handed over.
What should be agreed about operator loading before a bottle infeed machine is quoted?
Agree where bottles come from, how they are replenished, the normal loading pattern, the bottle condition at loading and the access available around guards and controls. The loading method can change bottle crowding, static, overlap and replenishment demand, so it should be part of the bottle trial rather than left as an operator assumption. Use the operator loading and access guide to prepare the brief.
What should be handed to production after a bottle unscrambler is commissioned?
Production should receive the approved bottle list, machine and guide settings, change-part references, normal loading method, stop and restart sequence, jam-clearance boundary, cleaning and inspection checks, trial evidence and any open items. The record should make the accepted operating condition repeatable across shifts. The production handover guide provides the structure.
What should a plastic bottle unscrambler demonstrate?
Test the bottle formats in their normal delivered condition, including lightweight or easily marked examples. Record correctly oriented bottles accepted by the downstream conveyor, not simply the discharge count. Include hopper replenishment, fallen bottles, blocked discharge and format changeover when assessing the feeding arrangement.
Measure acceptable bottle delivery at the line entrance
An unscrambler should be assessed by the bottles the next machine can accept. Define the required upright attitude, orientation, spacing and transfer condition at that handover. Then compare the automatic and rotary routes using the same bottle samples and demand pattern. The number of bottles moving on a disc is less useful than the number delivered correctly without intervention.
Separate the need to orient bottles from the need to accumulate or feed bottles that are already upright. The starting presentation changes the task. Show how containers arrive from storage, how an operator loads them and whether they can be tipped in bulk. This prevents a simple feed table and a fully orientating system being compared as though their scope were identical.
Review the least stable container and the most awkward production change, as well as the main format. A tall empty bottle, an offset shoulder or a narrow base may expose a different transfer requirement. Keep the line video, sample reference and agreed outfeed condition together so a later bottle change can be assessed against the original brief.
Start condition
Describe whether bottles enter randomly, upright, in trays or through manual placement.
Accepted outfeed
Record bottle attitude, travel direction, conveyor height and the receiving machine requirement.
Demand changes
Include downstream stops, restart and operator refill in the evaluation.
What is a useful bottle-feeding performance measure?
Count correctly delivered bottles at the agreed transfer point and record interruptions, rejects and operator corrections under the defined trial conditions.
Should the empty and filled bottle be treated as the same handling task?
Describe both where relevant. The unscrambler normally receives empty bottles, while later line stages may handle a different weight and balance.
Specification support
Send the bottle format and line speed. Get a sensible machine shortlist.
Lancing UK can advise whether a compact rotary unscrambler, automatic bottle unscrambler or wider line-infeed package is the correct route.